Full Circle

We are delighted to report our new angle ring for boiler No. 799 has arrived on site at Ropley. The angle ring, together with the previously delivered new tube plate, were funded by member donations to our boiler appeal. The ULS is very grateful to everyone who has supported this part of the project, which was over and above the original scope of the boiler’s overhaul.

Although these key components are now fully funded we are not resting our our laurels. Our new appeal is to fund the machining of 499’s coupling rods. We are targeting £5,000 to fund this work and will commence fundraising at this weekend’s Watercress Line Gala. The unmachined coupling rods have been in storage for many year so we are hoping to fit them shortly after the loco has been rewheeled. Any donations, large or small, are very much appreciated and this will be a lovely part of the project to tick off. Alternatively, why not visit out sales stand for some merchandise to help give 499 ten coupled wheels once more!

More engineering progress on 499 and our tender from around Ropley is below:
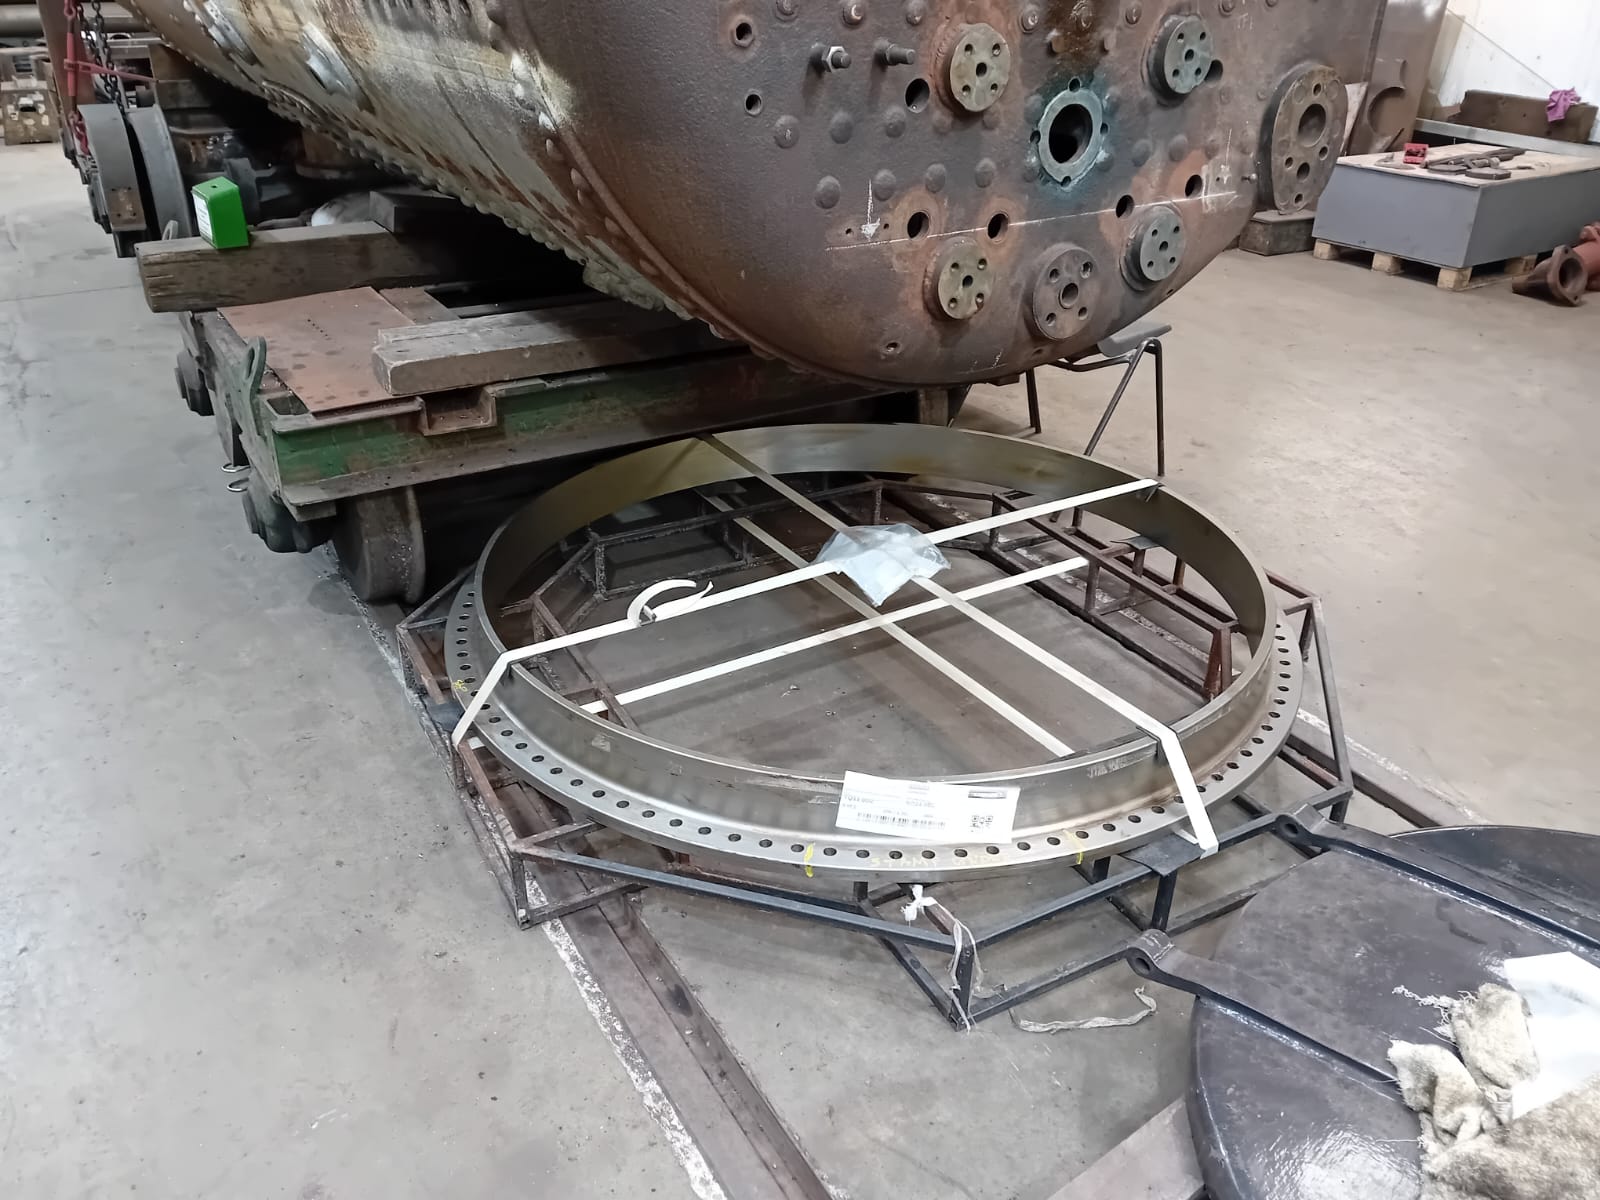
The brand new angle ring for boiler No. 799 has arived from our friends at the South Devon Railway who have machined it to fit the boiler barrel. Our boiler has also been repositioned at the far end of the boiler shop during a recent shunt.
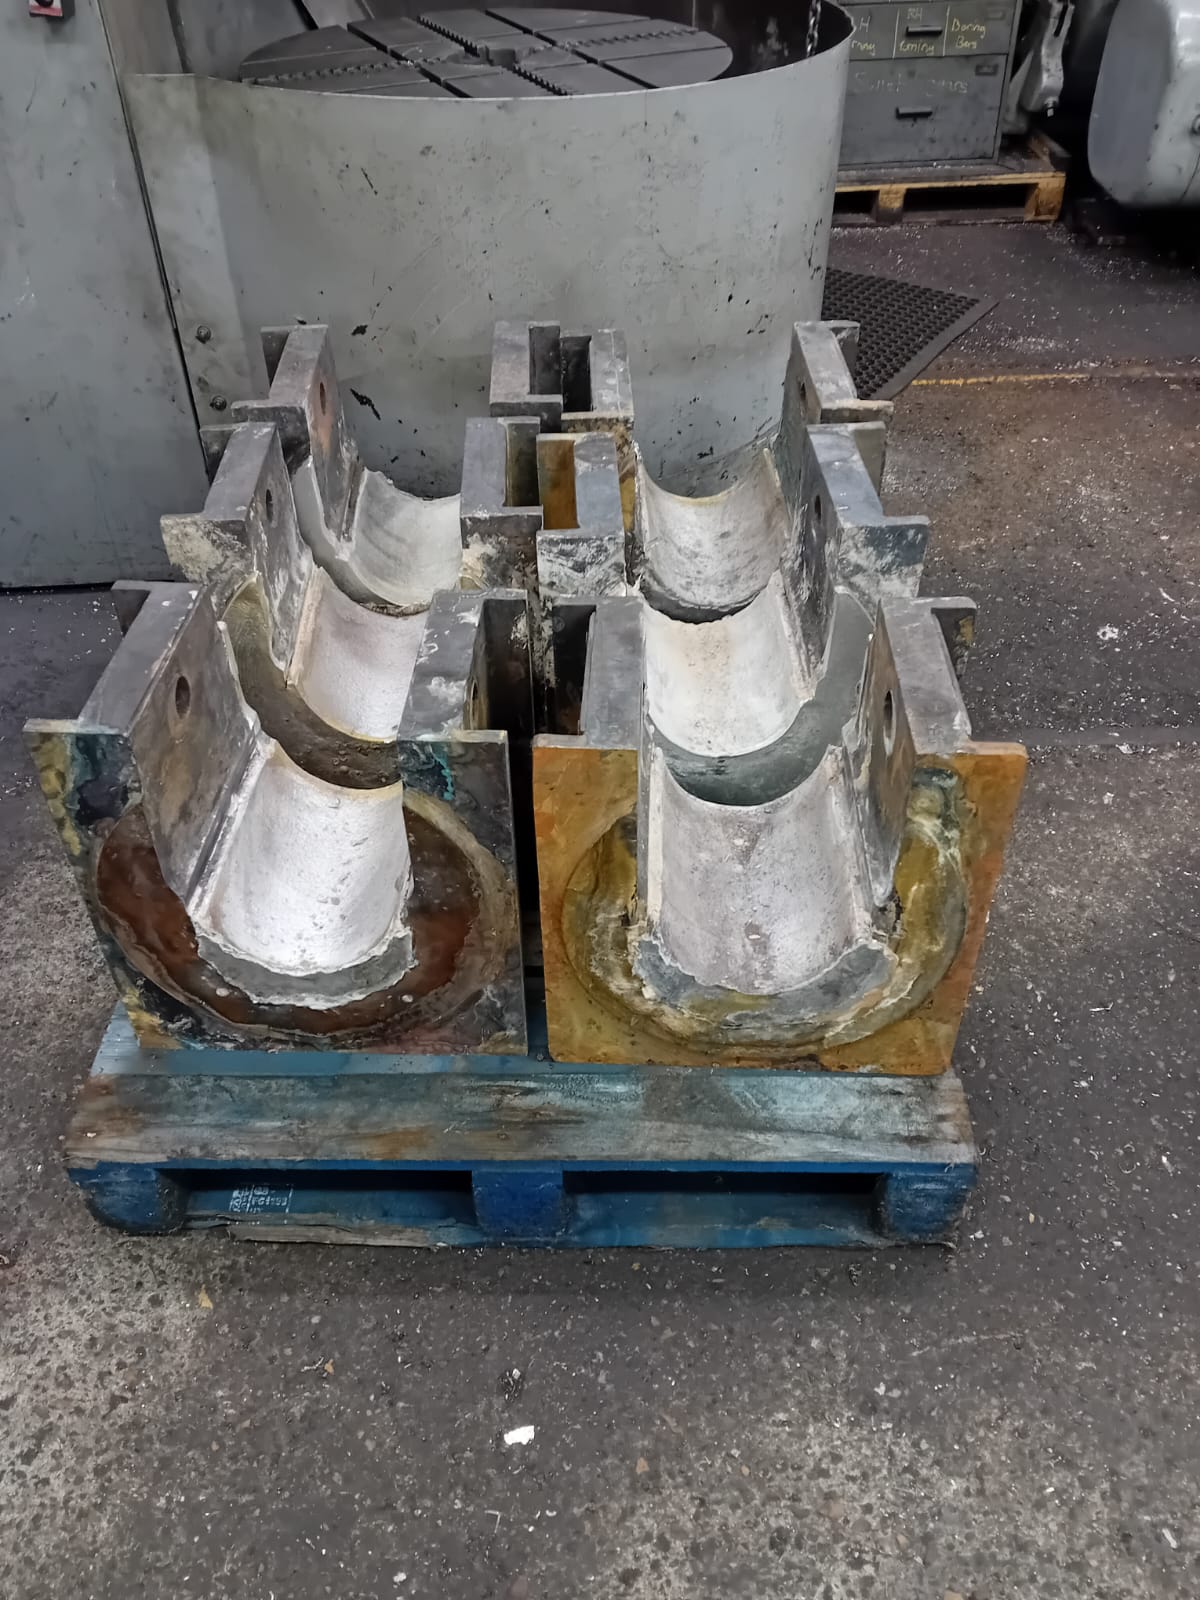
The Ropley staff have now white metalled all six of 499’s driving wheel axleboxes. These can now be machined to match the journals before final fitting.
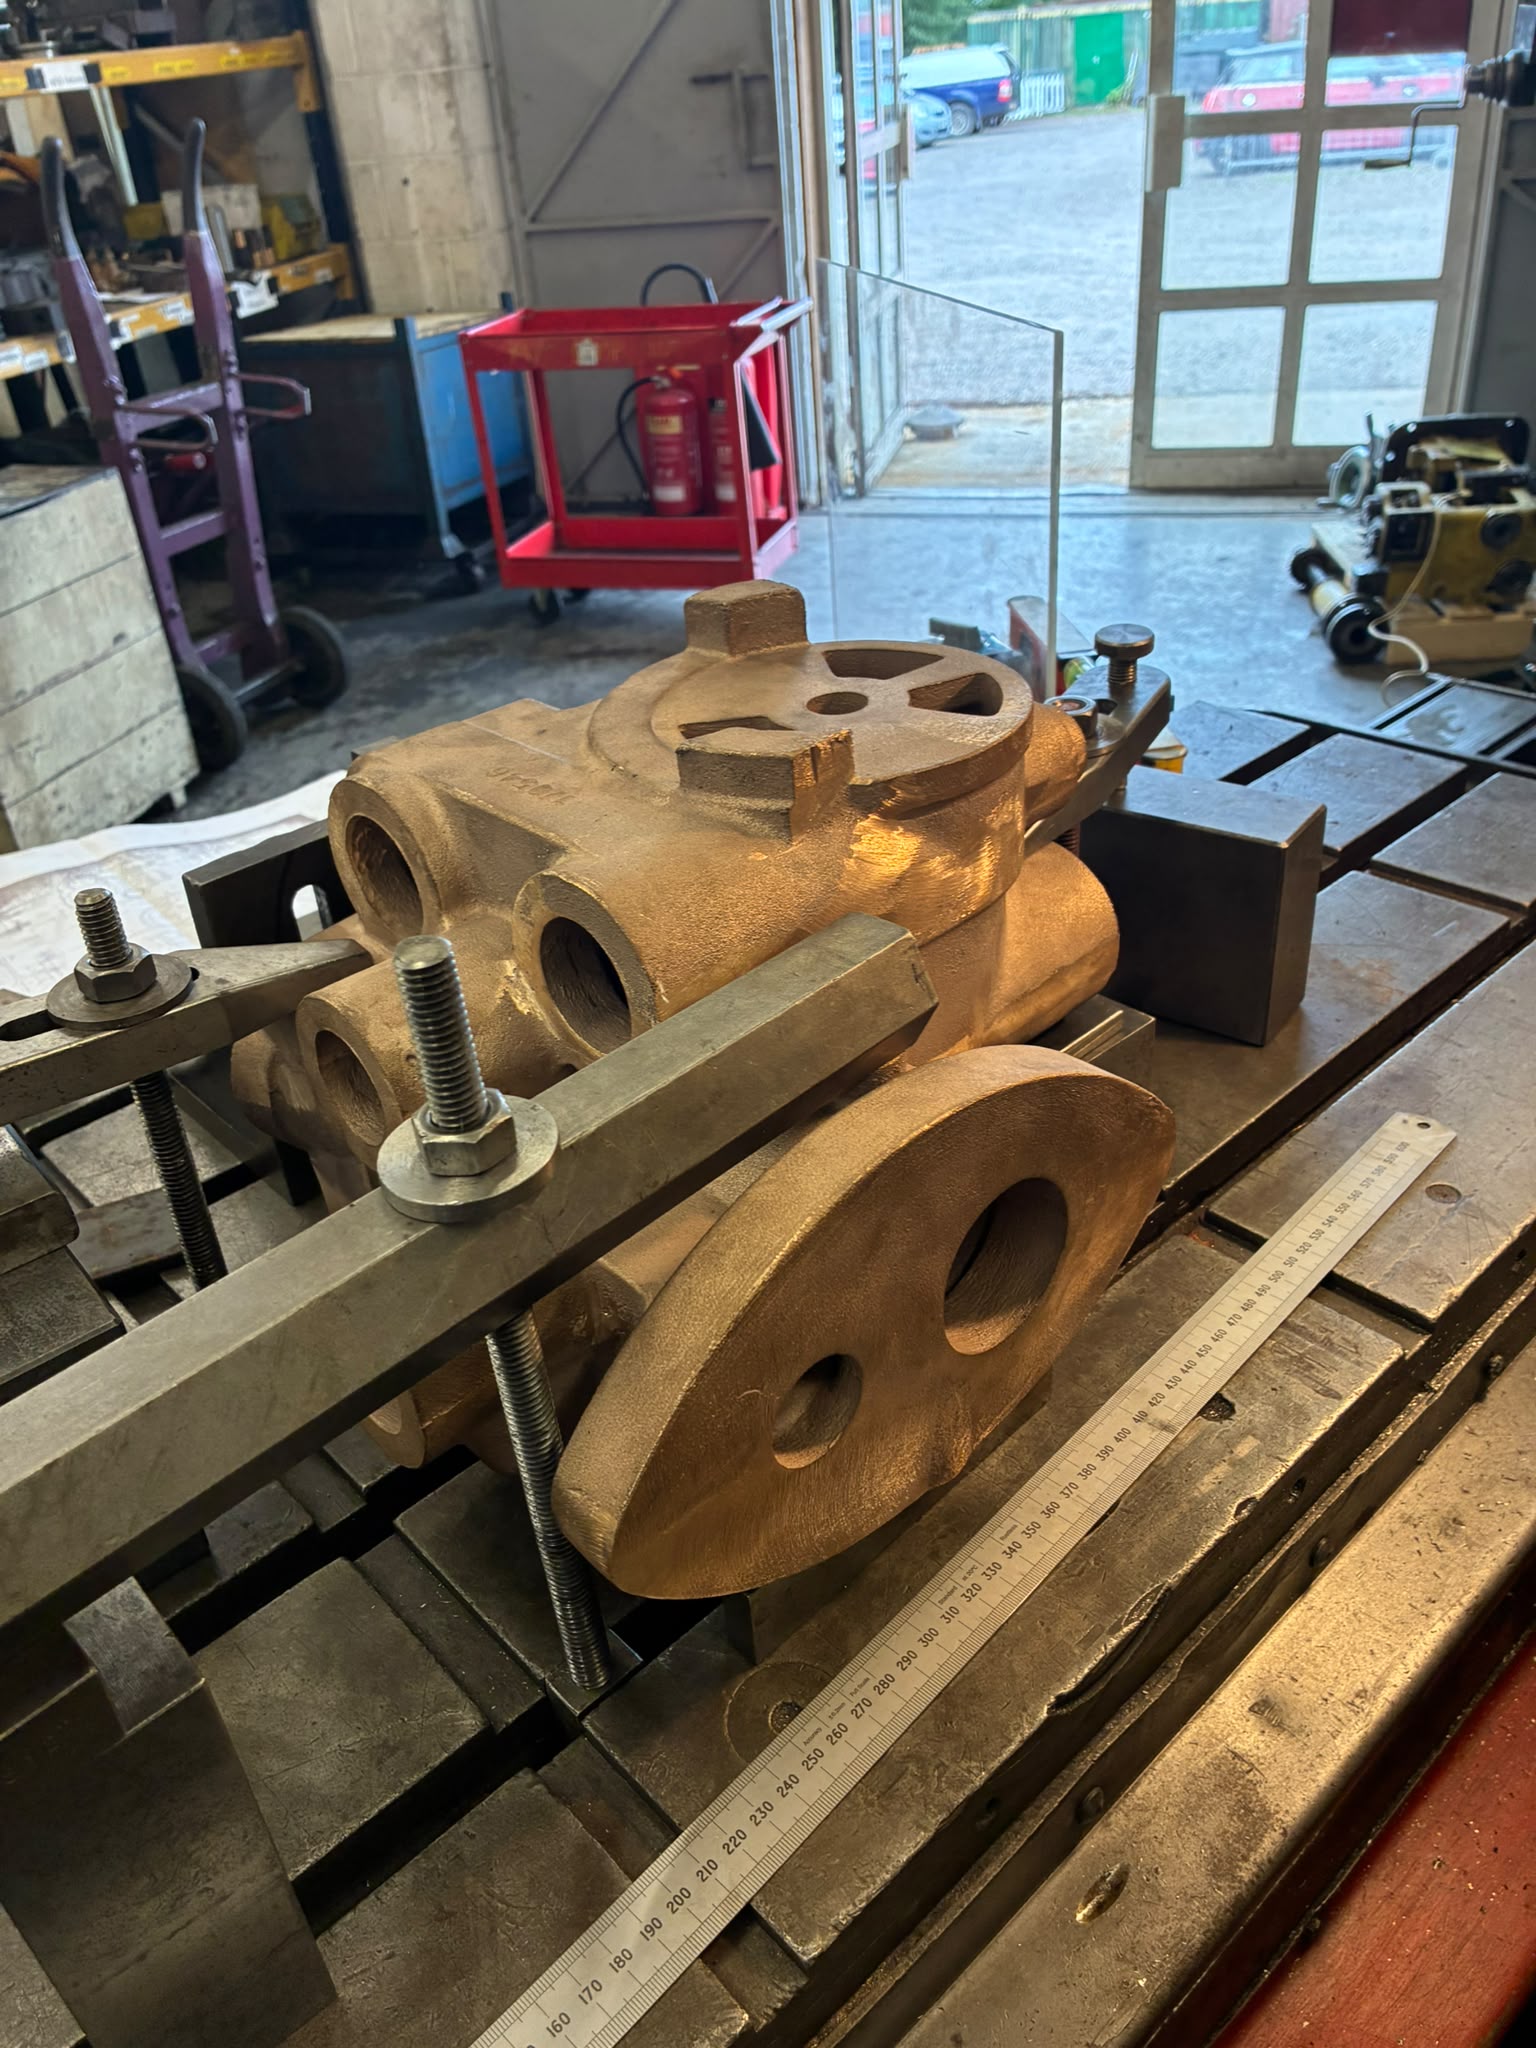
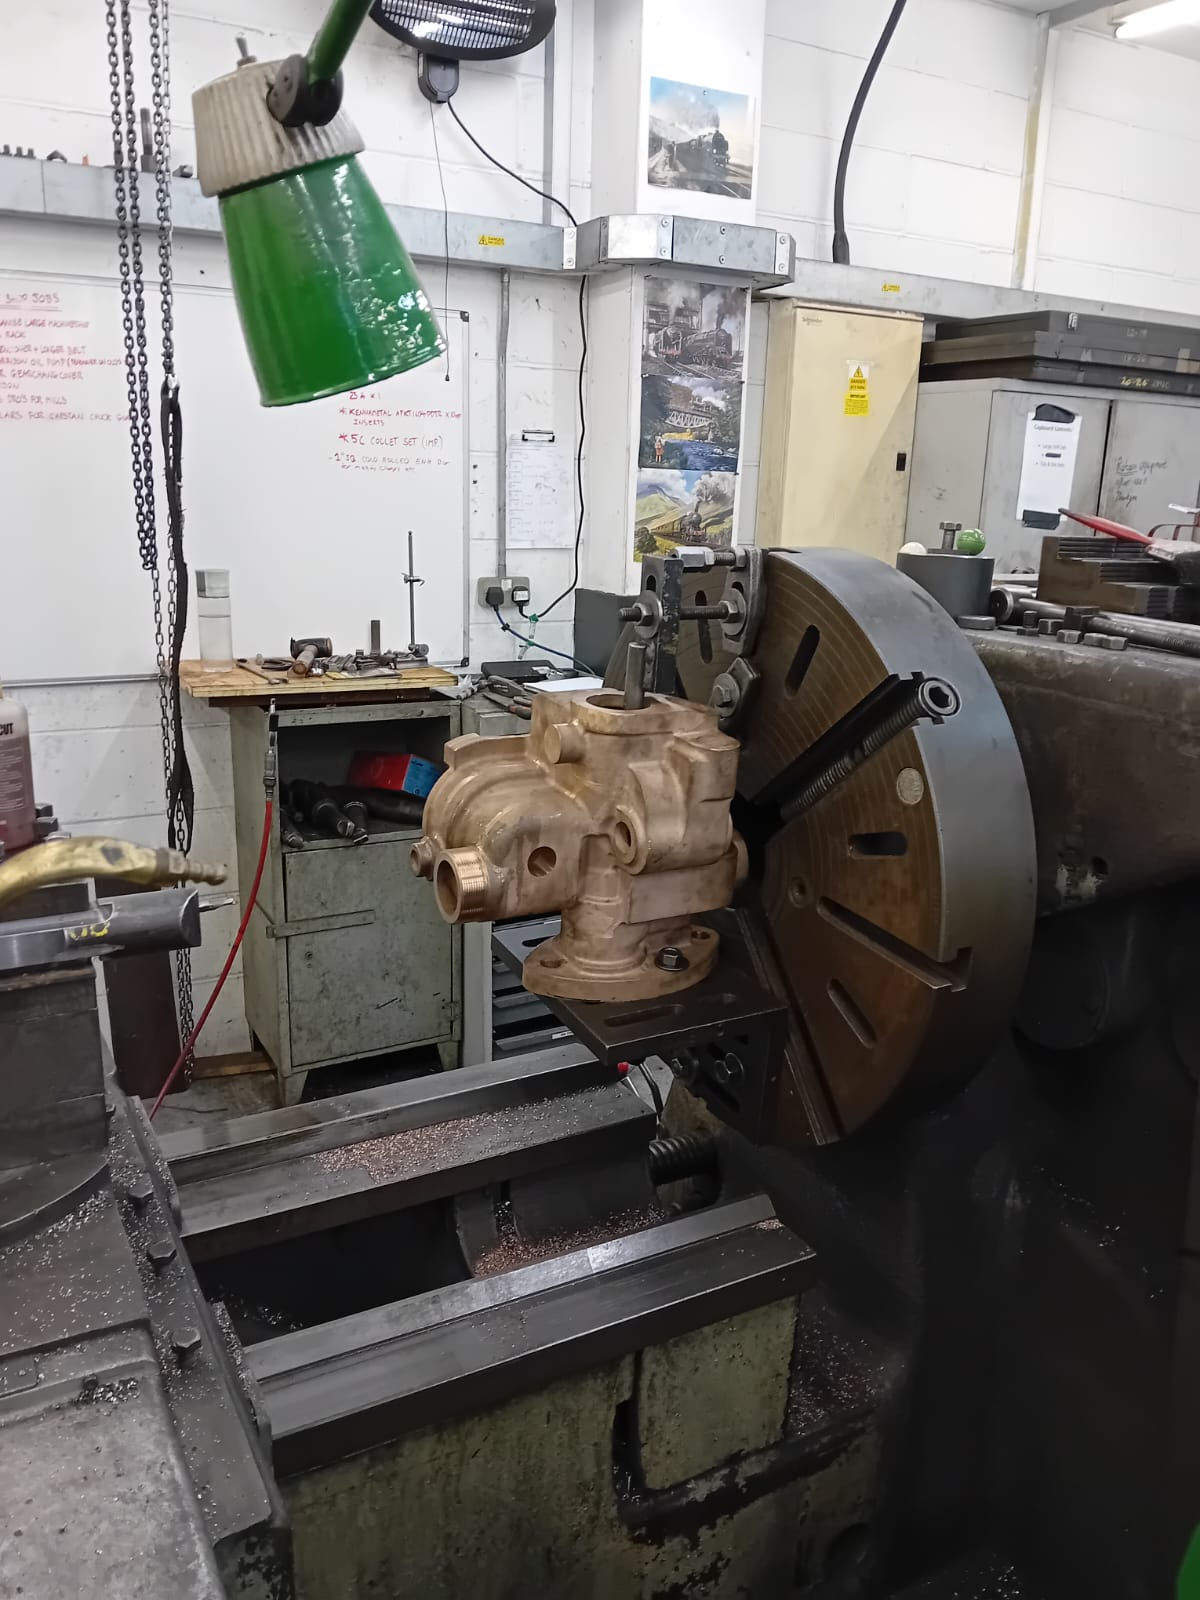
A start has been made on machining our new ejector casting. This will be a very time consuming process but it is crucial to prove that the casting itself is sound.
The new ejector casting in the Ropley machine shop.
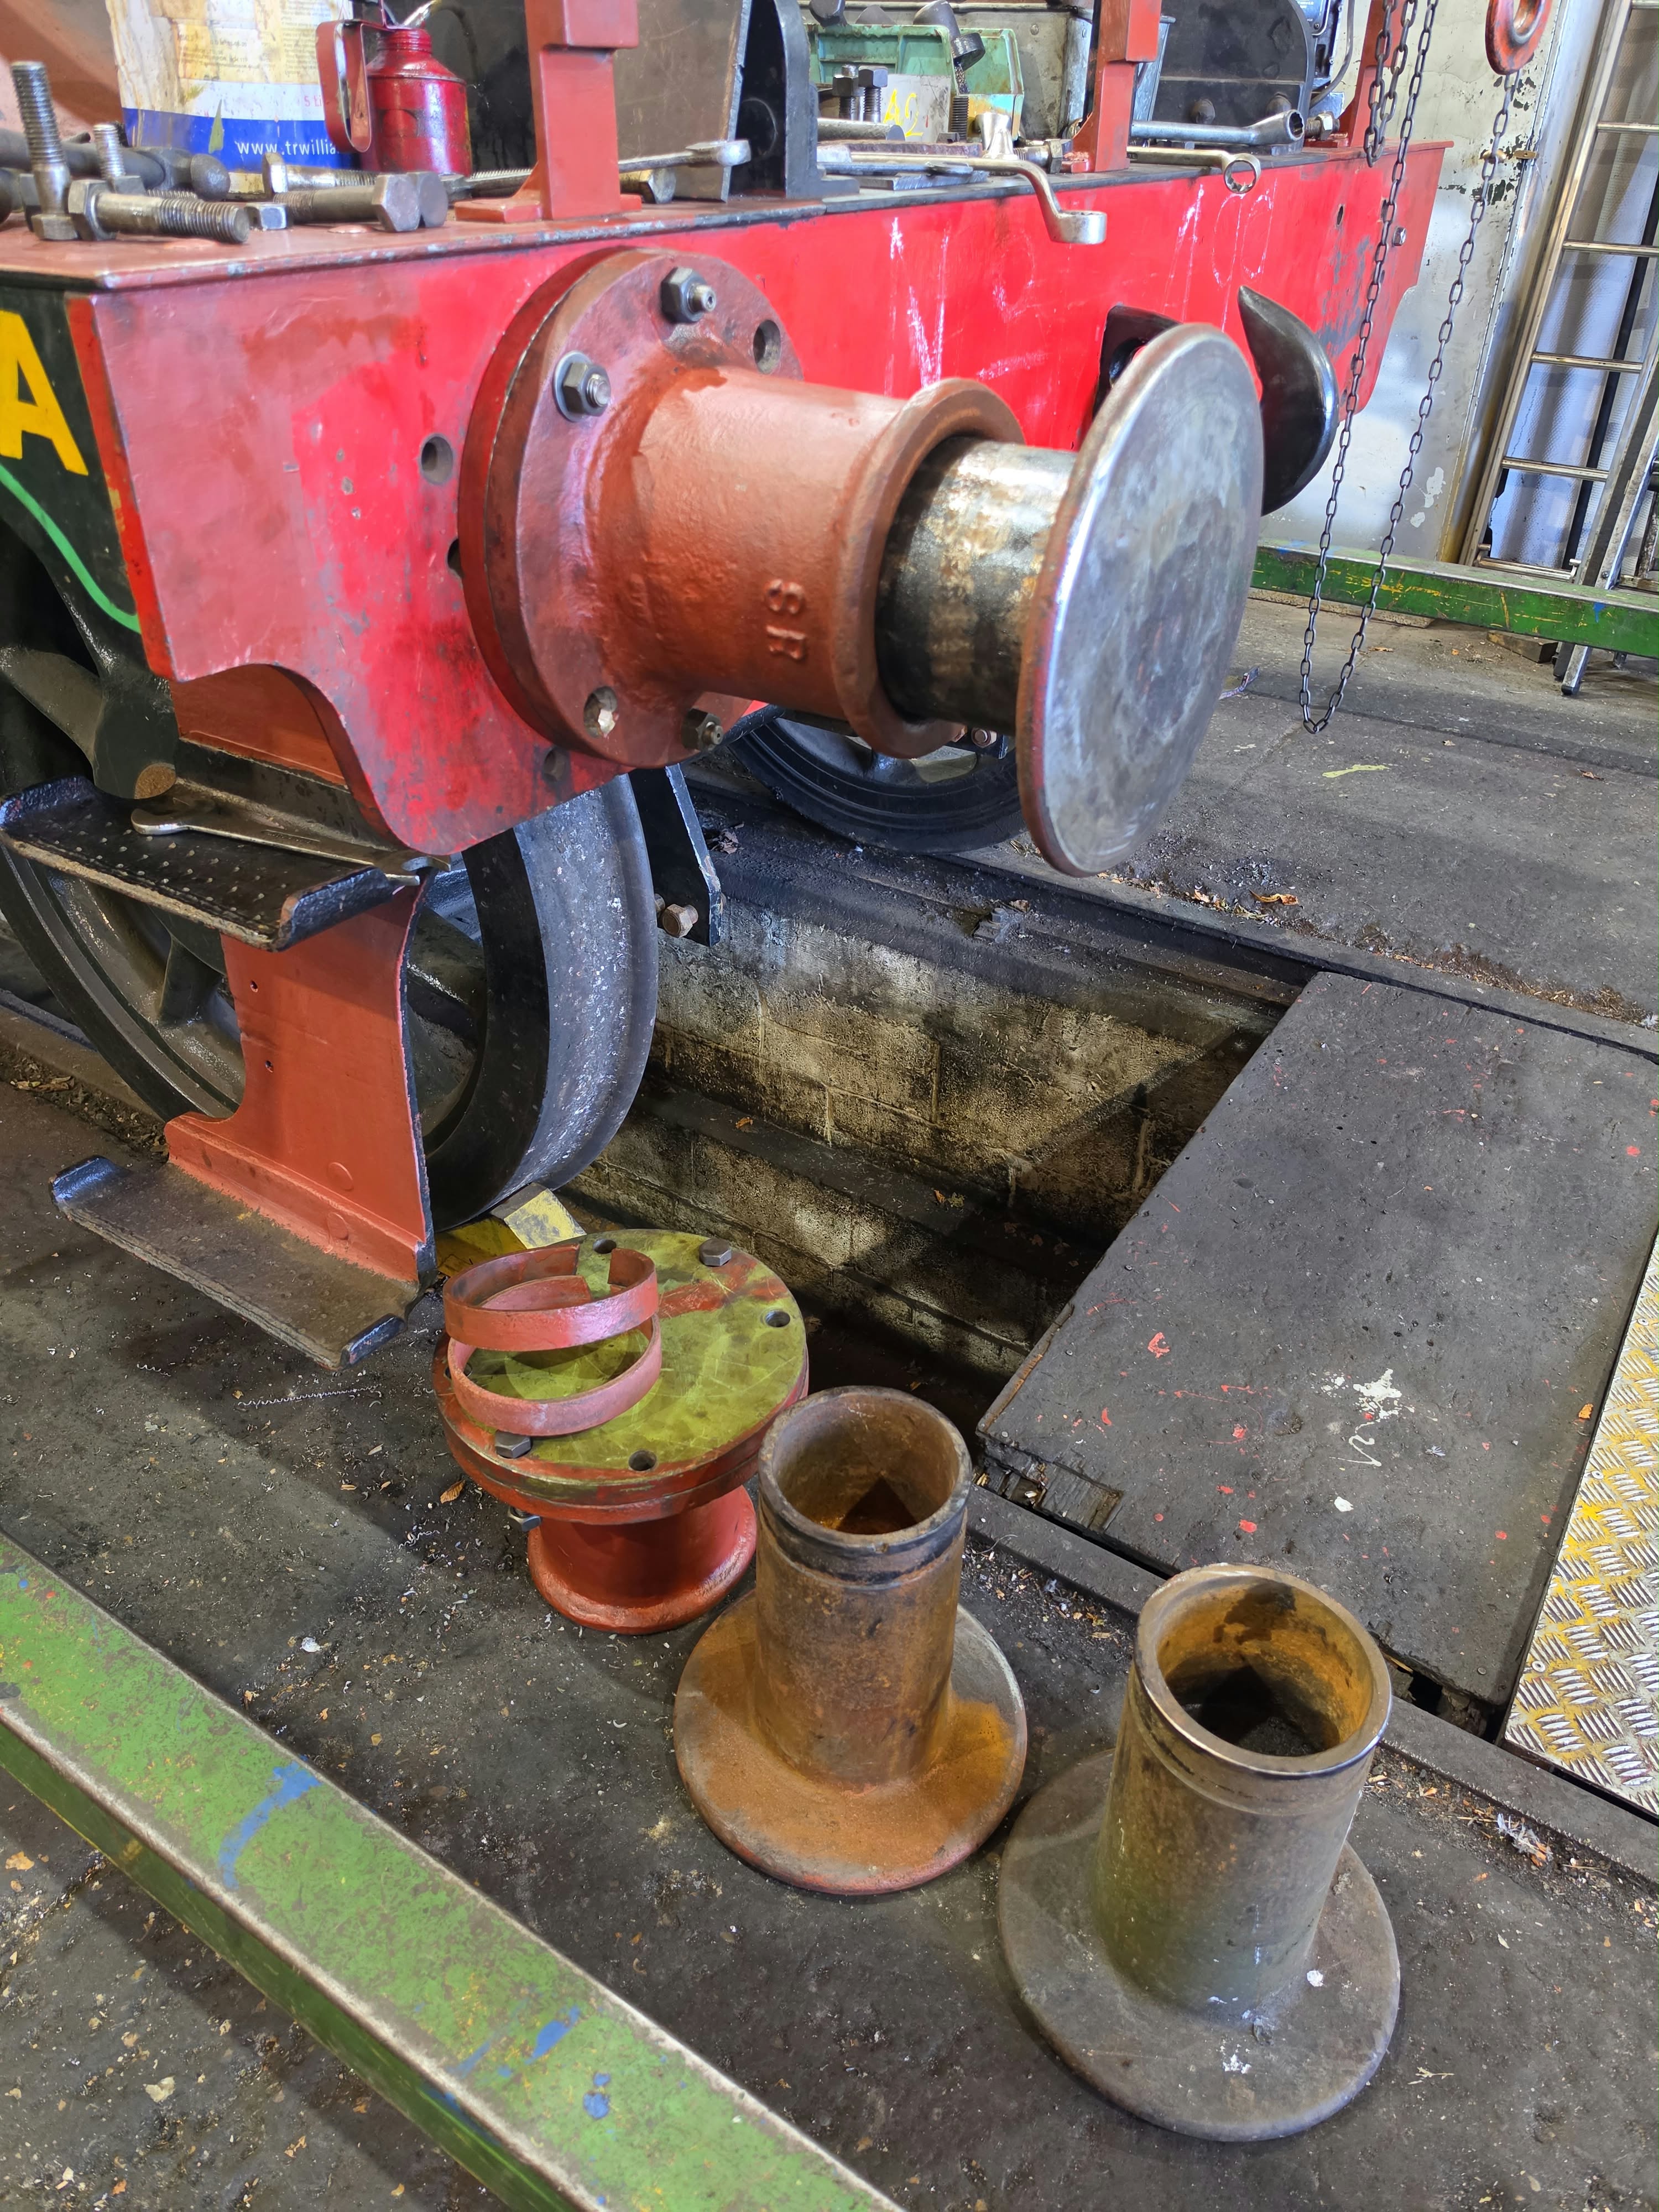
After some serious work in taking them apart we have set about assembling a collection of our best buffer components for the loco and tender. Here the first buffer has been trial fitting to the chassis. It will be removed to allow the steps to be riveted before final fitting.
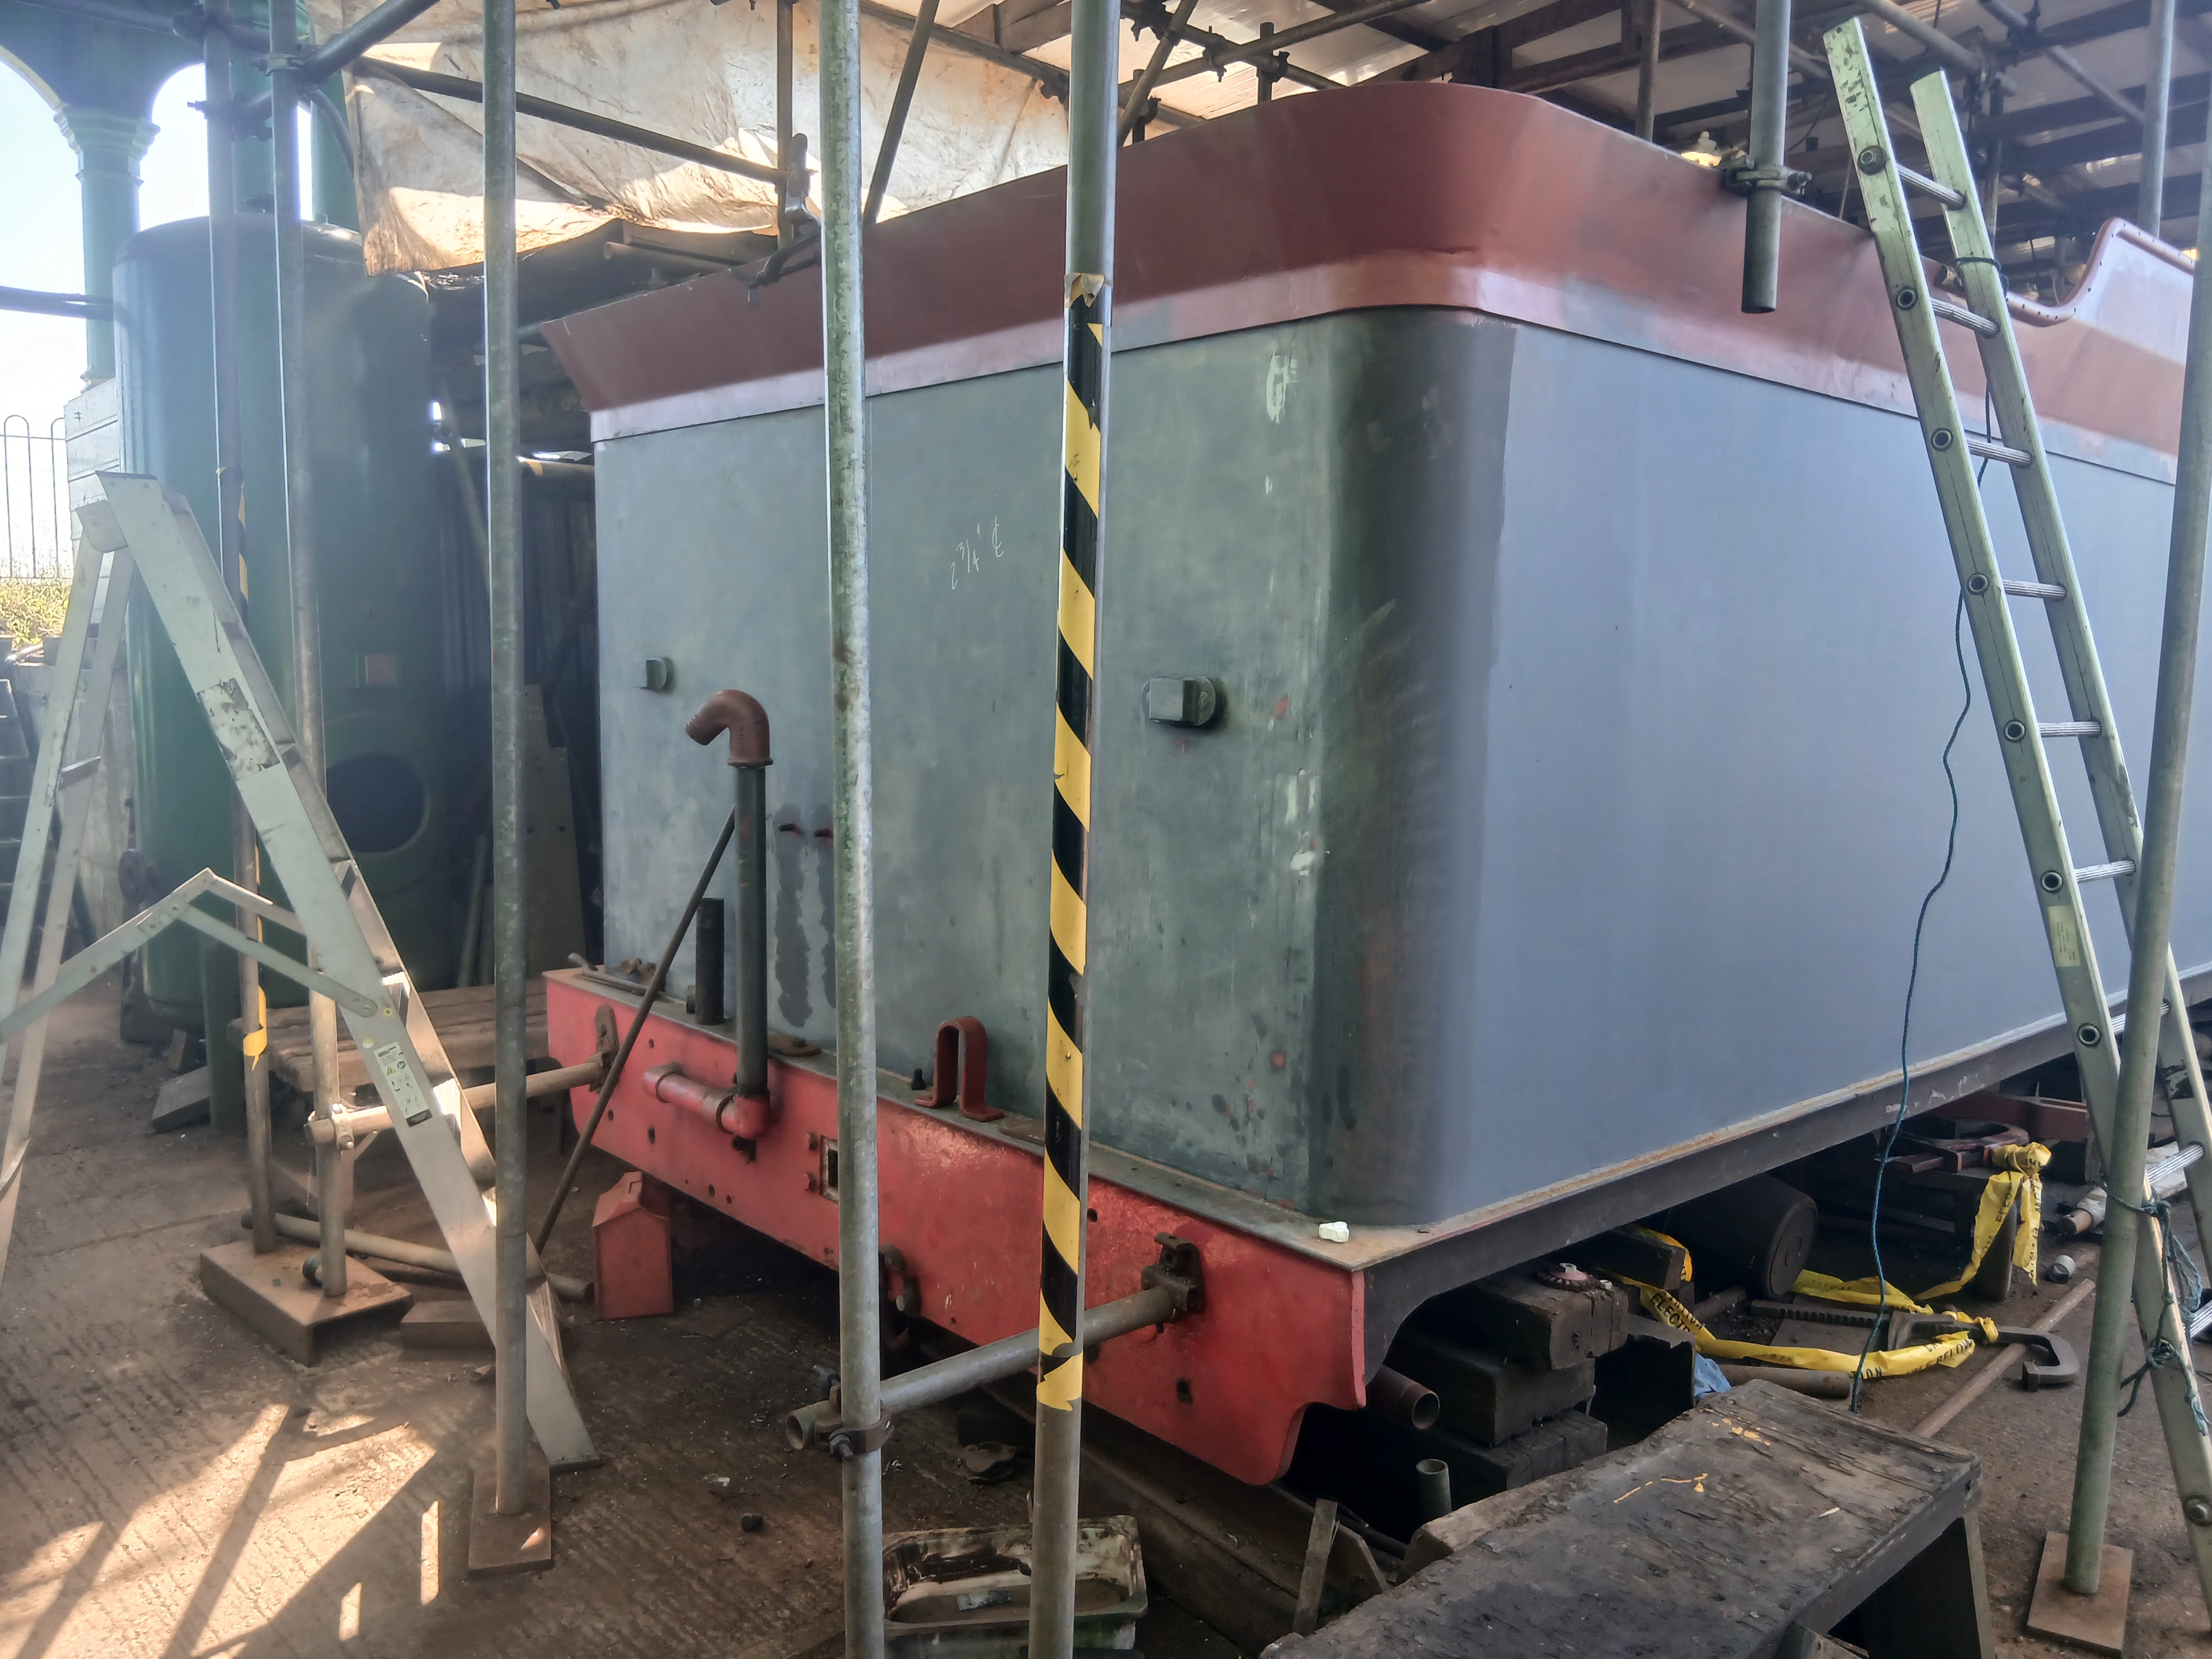
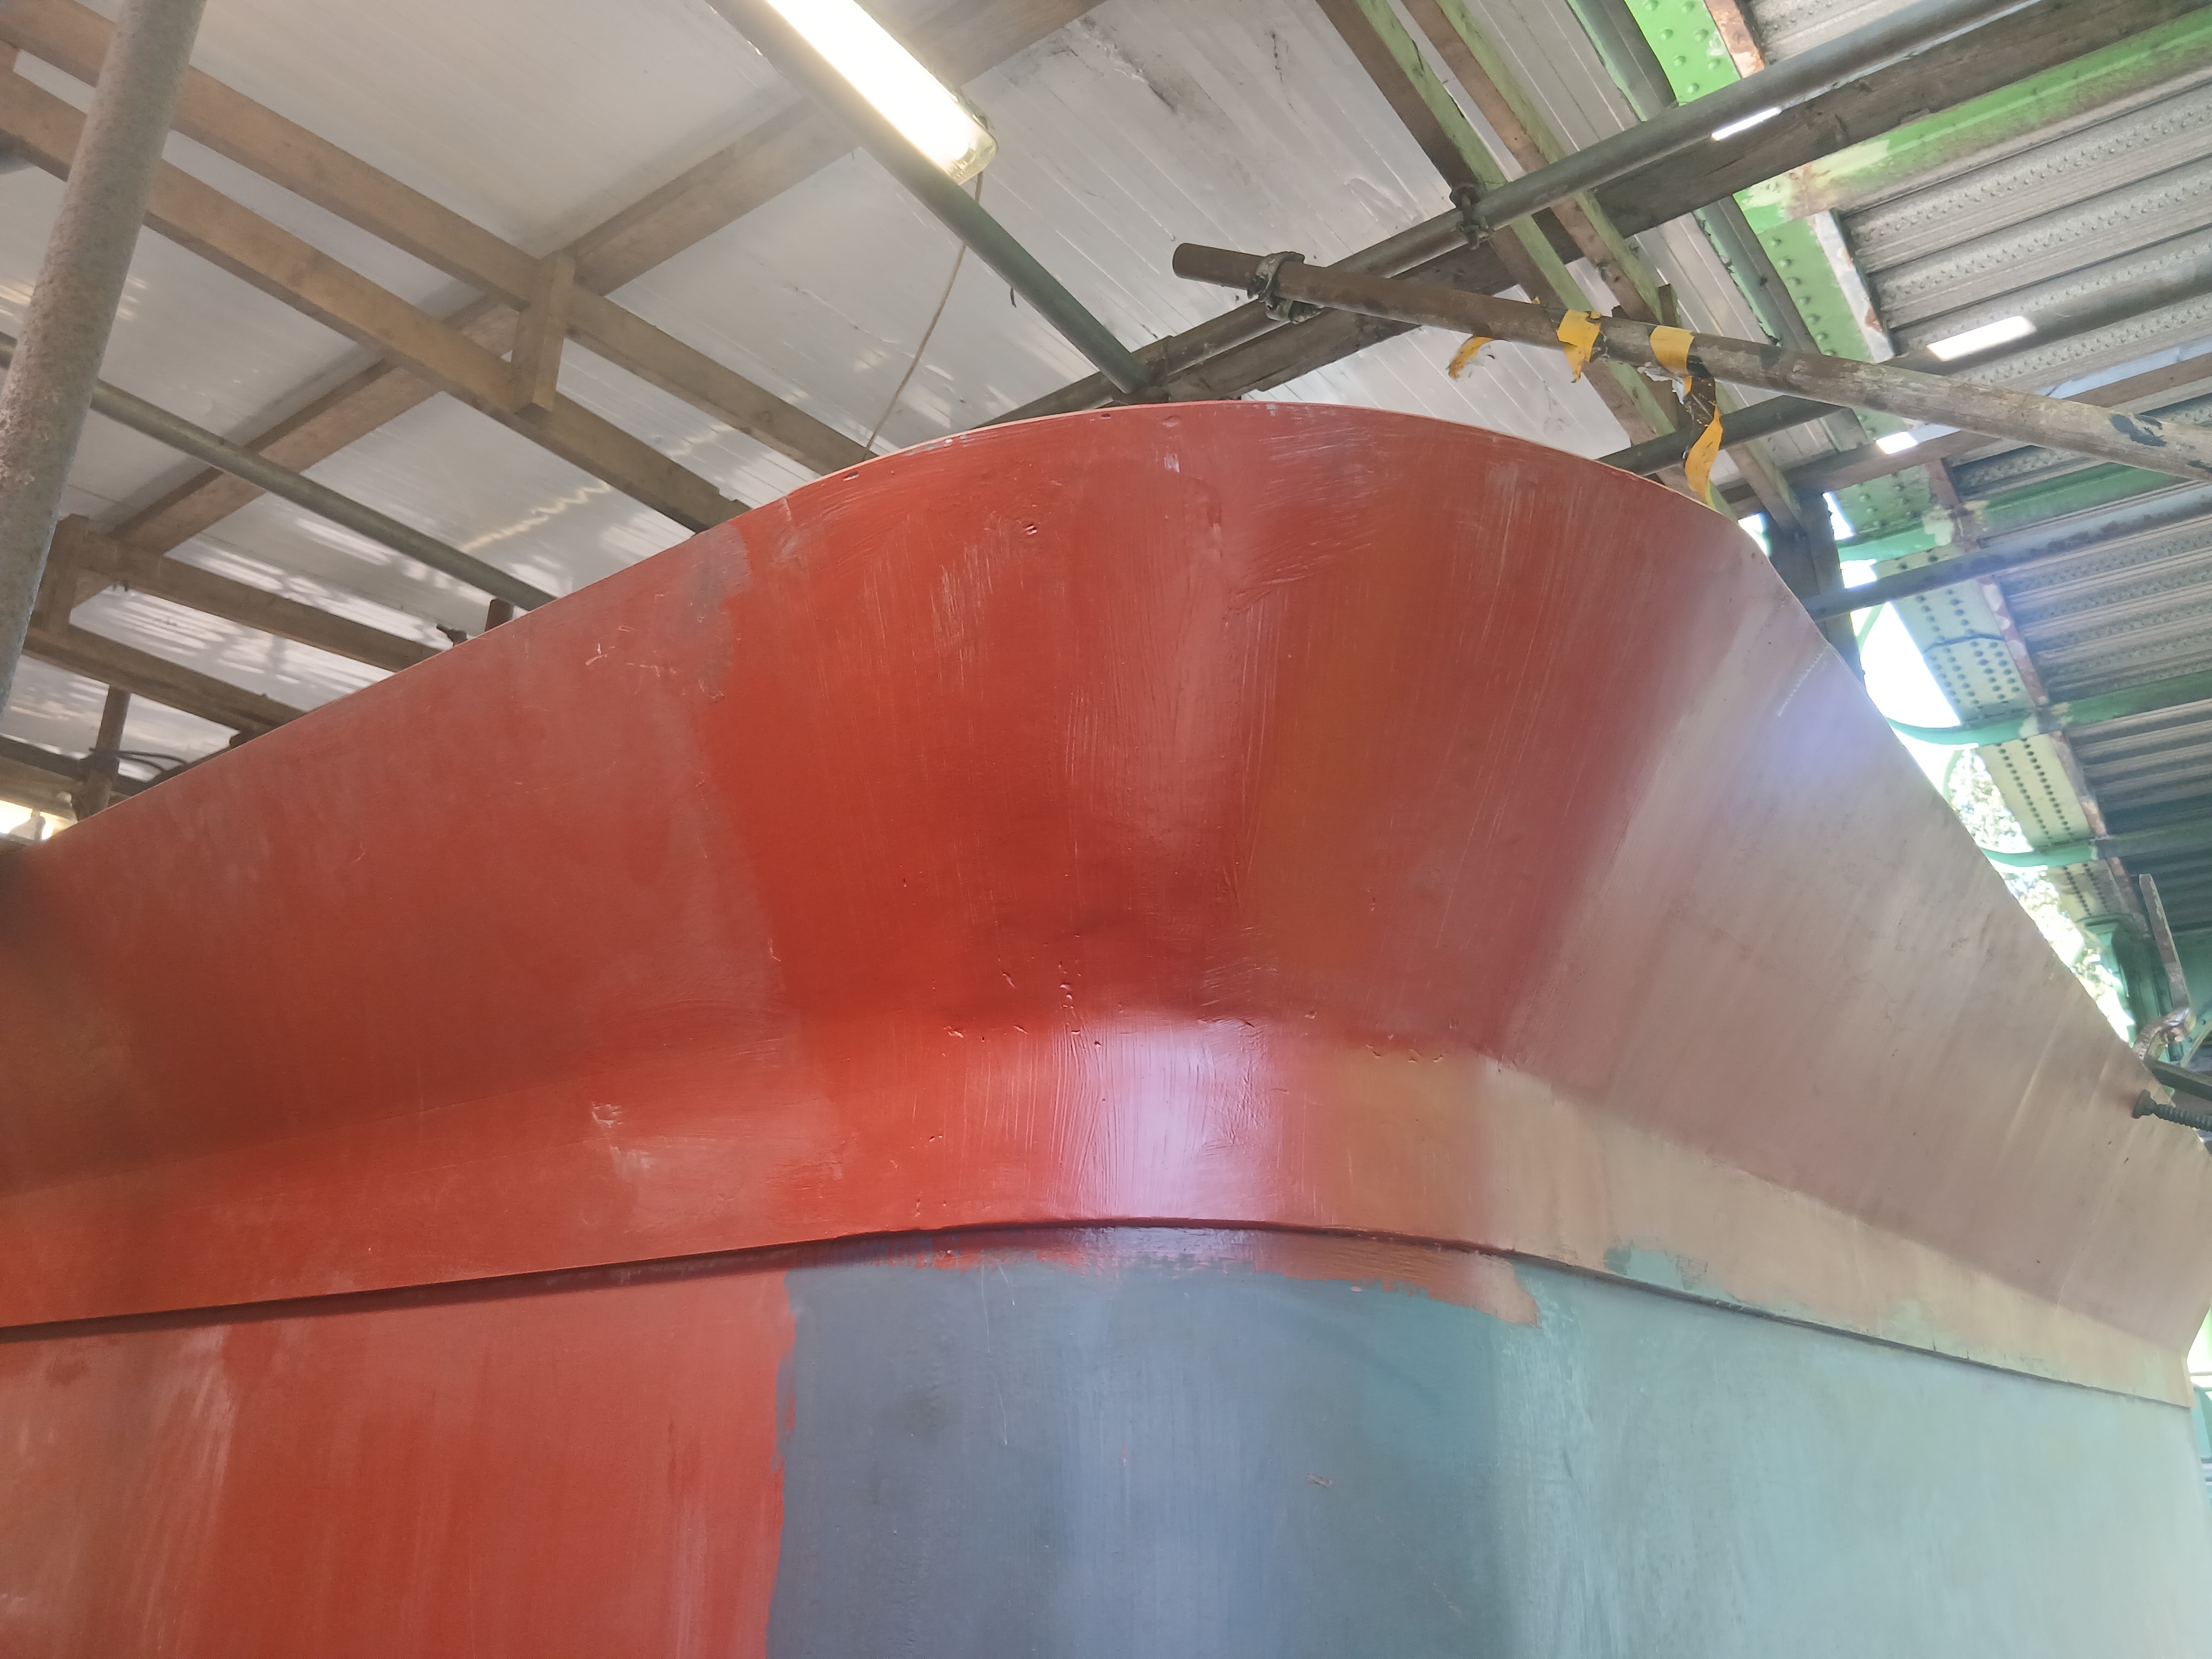
On the rear of the tender tank, we have now completed the curved sections of the raves and the next job will be to rivet on the beading.
Close up of tender rave corner section. We re-used a former that was left over from building 506’s tender tank to heat and bend flat steel to shape. A ready made process this time but still a lot of head scratching involved for Barry and the team. We are very proud of the result!
Share our posts